ALKA · AUSTRALIAN COATINGS MANUFACTURER
Industrial Pipelines
Define the external surface and the internal service.
SERVICE & APPLICATIONS
Protection matched to the asset.
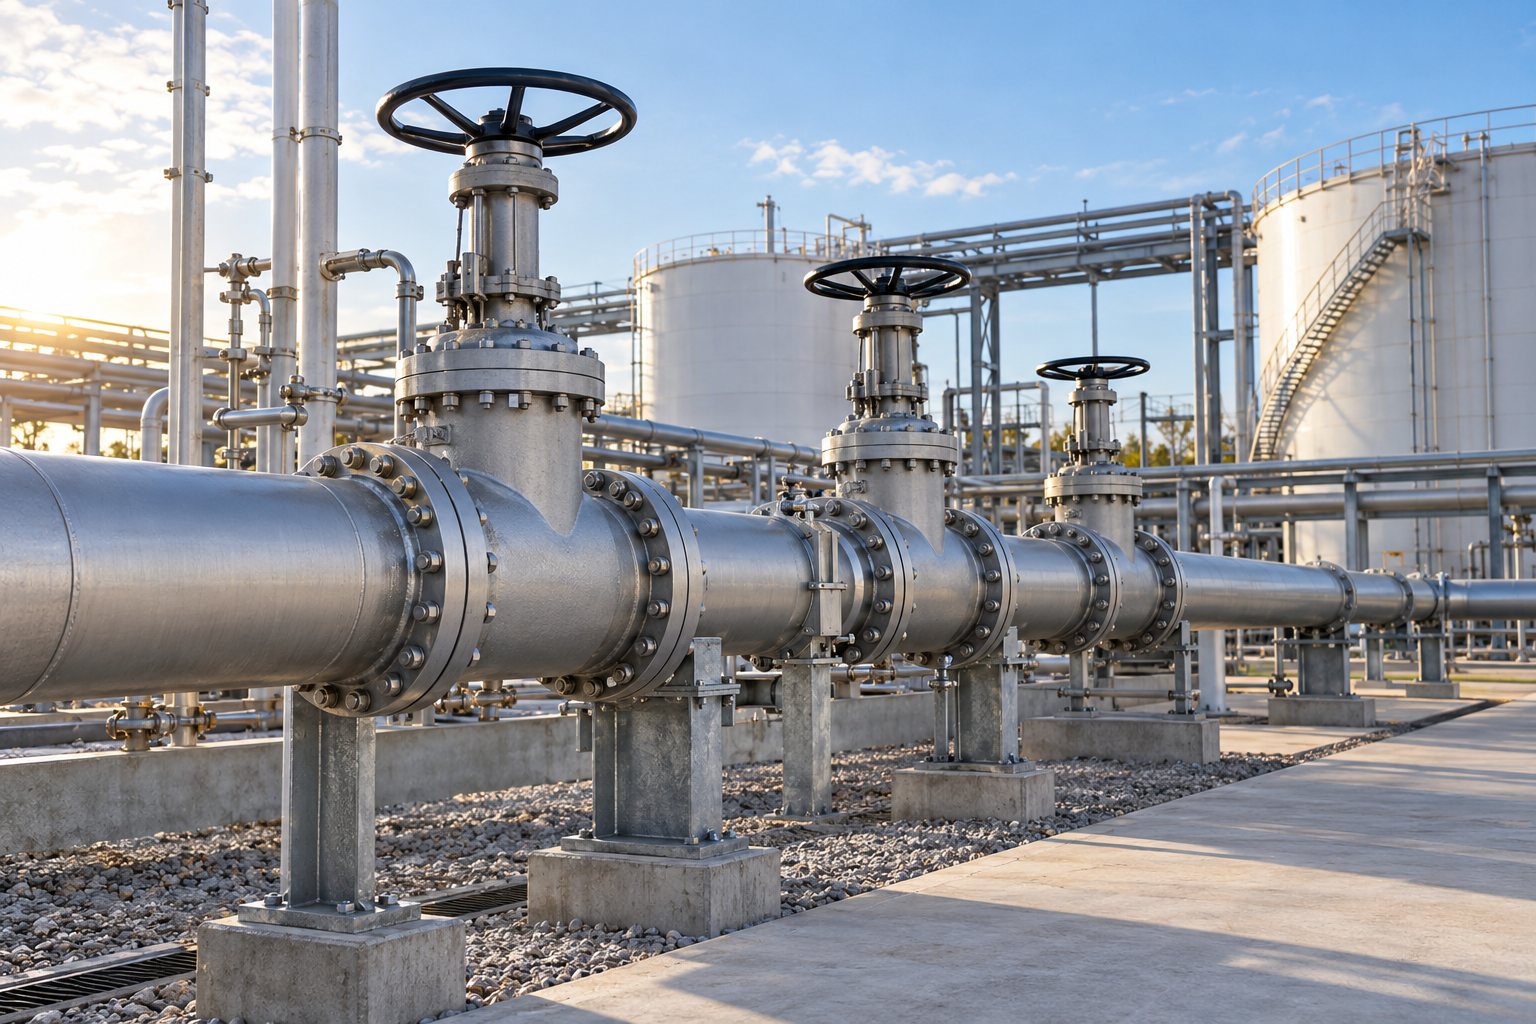
Pipework brings together different metals, operating temperatures and installation conditions. ALKA atmospheric and maintenance systems support prepared external steel and pipe supports, while internal linings follow a separate review of the conveyed material.
External pipe steel
Uninsulated above-ground surfaces need a build selected for atmospheric exposure and finish requirements.
Joints and supports
Specify weld repairs, transition edges and accessible inspection details around flanges and supports.
Lining duty
Chemical identity, concentration and temperature govern any internal chemical-lining selection.
ALKYD PRIMERS · ENAMELS · SINGLE-PACK FINISHING
Atmospheric finishes for selected pipework and supports
Single-pack primer/enamel finishes can be considered for suitable above-ground external pipework and support steel in ordinary atmospheric conditions. The external finish, internal lining, insulation and operating temperature must be reviewed separately before choosing the system.
Products to assess for the job
- ALKA 401 · Alkyd zinc phosphate primer
Prepared carbon steel; a corrosion-inhibiting primer for compatible alkyd and enamel finishing routes.
- ALKA 403 · Red oxide anti-corrosive primer
A primer option for prepared ferrous metal, fabricated steel and general maintenance; confirm the selected finish compatibility.
- ALKA 410 · Rapid-cure protective enamel
A gloss finishing option for machinery, fabricated components and maintenance work over a compatible prepared and primed surface.
Select a complete, compatible primer and finish. The products above are options by role, not a blanket approval to combine every primer and topcoat.
What the applicator or specifier needs
Define the service by line and component, including temperature, insulation, spills and cleaning. Agree identification colours and markings with the project requirements.
Inspect clamps, saddles, welds and crevices before specifying spot repairs. Remove contamination and confirm the soundness and compatibility of retained coatings.
Plan inspection and repair at support interfaces and after assembly. Confirm the required cure before process temperature or cleaning affects the coating.
Write a usable coating schedule
Specify the substrate and preparation, exact primer and finish, individual-coat dry-film thickness, application method, thinning limits, recoat interval and service-cure requirement from current product data. For repainting, document the retained coating and a representative compatibility trial before full application.
Choose the coating for the exposure
Internal fluids, burial, insulation-related corrosion and high-temperature service require separate specifications.
A single-pack route can simplify small batches and routine repainting because it does not require mixing a separate hardener. It still depends on sound preparation, suitable film build and the correct recoat window. Where exposure or the required maintenance interval is more demanding, assess the relevant two-pack epoxy, polyurethane or specialist lining system.
Does fast drying mean the part is ready for service?
No. Touch-dry, recoatable, handleable and fully cured describe different stages. Use the selected product data and actual application conditions to plan each stage. Excessive film build, early overcoating or premature handling can compromise the finish; adding extra thinner or a hardener is not a substitute for the specified application procedure.
SELECT THE COMPLETE BUILD
ALKA systems for this application.
| System | Why select it | Coating build | Total DFT |
|---|---|---|---|
| ALKA-9930 Premium External | Premium corrosion protection combined with a UV-stable, colour-retentive finish Abrasive-blasted carbon steel; external industrial and coastal atmospheric exposure | Alka 404 zinc-rich epoxy primer → Alka 413 high-build epoxy → Alka 421 polyurethane finish | 250–300 µm |
| ALKA-9932 Maintenance / Refurbishment | Reduces preparation demands and supports practical maintenance programs Existing steel where full abrasive blasting is restricted; hand- or power-tool prepared areas | Alka 412 surface-tolerant epoxy × 2 coats → optional Alka 421 polyurethane finish | 200–400 µm plus optional 50–75 µm finish |
| ALKA-9936 Chemical-Resistant Lining | Higher chemical resistance than standard epoxy systems for demanding process environments Prepared steel or concrete in tanks, bunds, process areas and secondary containment | Alka Tanklin 100 and/or Alka Tanklin Chem system selected to suit the chemical service | 450–600 µm |
DFT = dry-film thickness. These are nominal system totals; individual-coat thicknesses and application conditions belong in the final coating schedule.
SPECIFICATION & APPLICATION
From surface preparation to return to service.
Build the coating schedule around the substrate and the work that can be achieved on site. For refurbishment, assess the adhesion and compatibility of retained coatings before defining repair boundaries.
- 01External or internal surface
- 02Operating temperature range
- 03Buried, exposed or insulated
- 04Conveyed material and maintenance access
Record surface preparation, environmental conditions, coverage at details and coat thickness. Allow for the specified recoat and cure periods, then inspect and repair defects before release to service.
ALKA-9930 · External steel example
Schematic, not to scale. Follow the selected system for products, layer count and thickness.
TECHNICAL QUESTIONS
Details that affect system selection.
Why distinguish insulated pipework?
Insulation changes the environment at the coating surface and can involve temperature cycling and retained moisture. Provide the operating range and insulation details for a dedicated coating assessment.
What belongs in the final technical submission?
Include current TDS and SDS, substrate preparation, the product and thickness schedule, application conditions, inspection criteria and cure requirements. For chemical or immersed service, include written suitability for the actual exposure. Any required certification or durability commitment must be supported by the relevant evidence.
Buried service, cathodic protection, insulation and elevated or cryogenic temperatures are not covered by a general external paint selection. Define these as separate duties.
PRODUCTS & TECHNICAL DOCUMENTS
Go directly to the product information.
Read the published technical data sheets below, or open a product overview. Request the current SDS set and confirm the document revisions for your specification before procurement.
MANUFACTURER TECHNICAL SUPPORT
Turn the service conditions into a coating specification.
Send the asset, substrate, exposure and maintenance window. ALKA can help define the coating build, preparation and technical documentation for your review.