BUILT ENVIRONMENT
Buildings & Structural Steel
Coating systems for exposed building steel, architectural metalwork and plant assets where protection and appearance work together.
ALKA PROTECTIVE COATINGS
Protect the steel. Define the finish.
Exposed steelwork needs a finish that fits the architecture and a protective build that suits its surroundings. ALKA manufactures coating systems for commercial and industrial building structures, fabricated components and maintenance steelwork.
External building steel
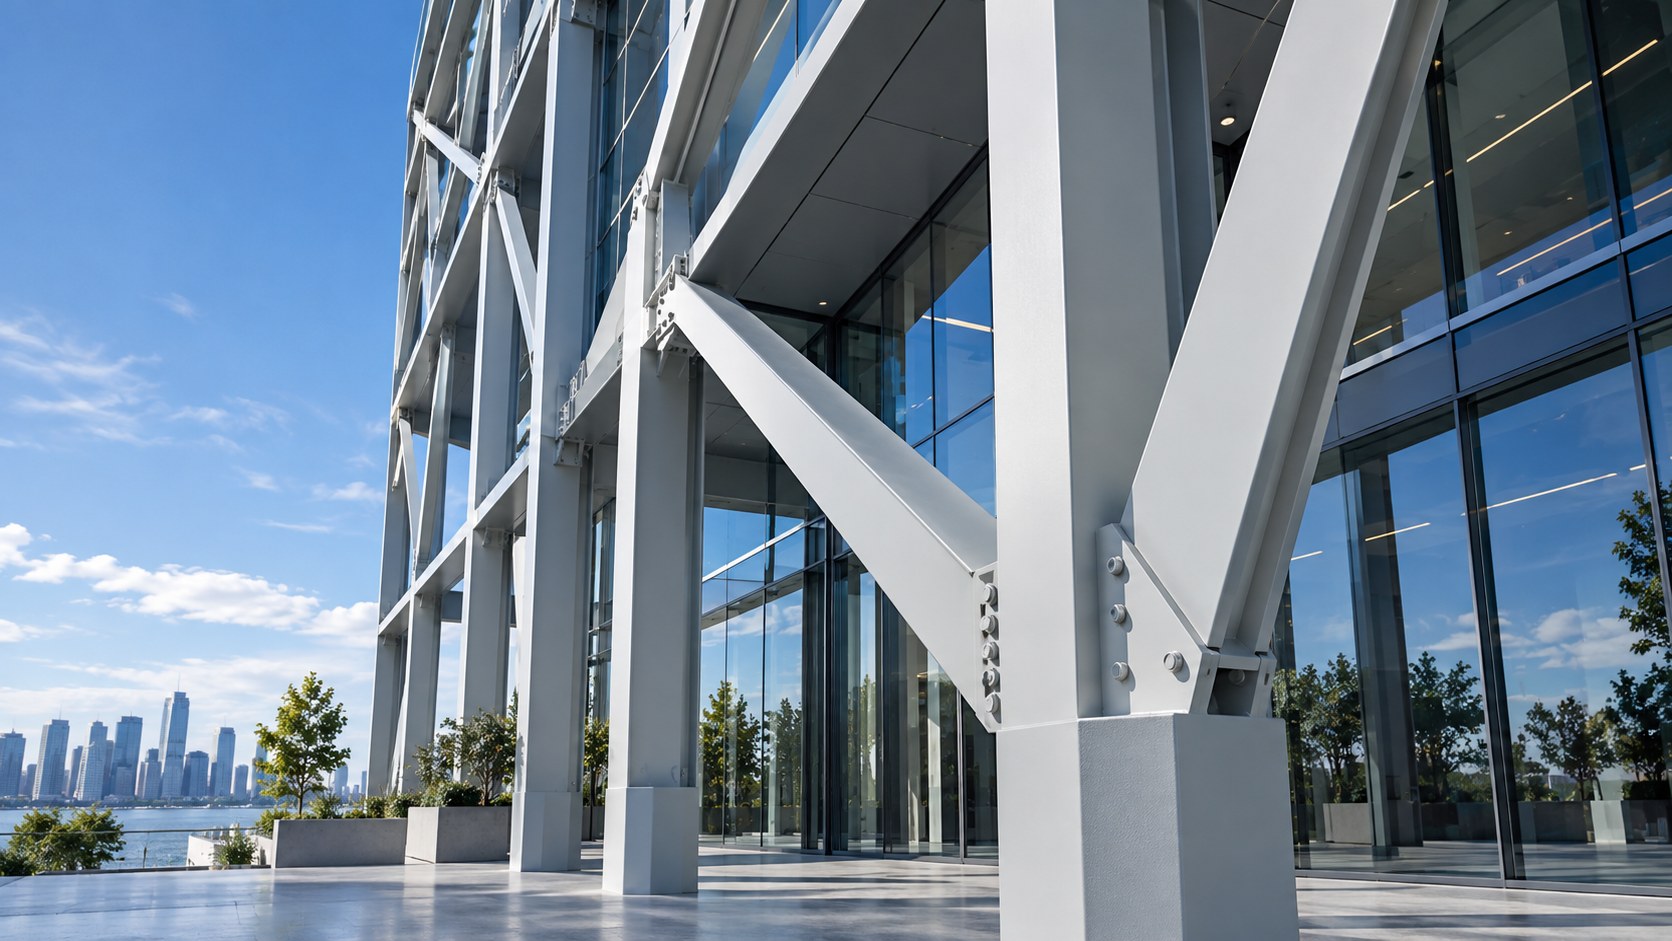
Columns, canopies, exposed frames and architectural steel subject to weathering and UV exposure.
Fabricated components
Doors, railings, frames and equipment with moderate atmospheric exposure and a specified colour and finish.
Internal and service steel
Equipment supports and internal structures where practical maintenance and a suitable barrier coating are the priority.
UNDERSTAND THE SERVICE
Balance architectural appearance with the exposure behind it.
External versus sheltered steel
A weather-facing canopy and an internal equipment frame do not have the same exposure. Separate locations in the finish schedule and identify coastal or persistently damp conditions that need a closer review.
Substrate and shop-coating interfaces
Fabricated steel may arrive bare, primed or galvanised. Record the actual substrate and existing coating before selecting a primer; an assumed shop-primer compatibility can undermine the complete finish.
Appearance through fabrication and erection
Colour, gloss and texture should be agreed with a representative sample. Define repairs to handling damage, site welds and connections so shop-applied and site-applied work have a coordinated finish.
ALKYD PRIMERS · ENAMELS · SINGLE-PACK FINISHING
Alkyd primers and enamel finishes for building metalwork
Doors, railings, gates, frames, service cabinets and selected fabricated components can be considered for single-pack primer/enamel finishes. This gives building projects a practical metal-finishing route alongside the epoxy and polyurethane systems selected for more demanding structural exposure.
Products to assess for the job
- ALKA 401 · Alkyd zinc phosphate primer
Prepared carbon steel; a corrosion-inhibiting primer for compatible alkyd and enamel finishing routes.
- ALKA 402 · Single-pack acrylic etch primer
A substrate-specific adhesion option for steel and suitable galvanised or aluminium components. This is a thermoplastic acrylic primer, not an alkyd.
- ALKA 403 · Red oxide anti-corrosive primer
A primer option for prepared ferrous metal, fabricated steel and general maintenance; confirm the selected finish compatibility.
- ALKA 410 · Rapid-cure protective enamel
A gloss finishing option for machinery, fabricated components and maintenance work over a compatible prepared and primed surface.
- ALKA 415 · Hammer-tone finish
A decorative textured finish for machine covers, cabinets, enclosures and fabricated metal items where appearance is part of the brief.
Select a complete, compatible primer and finish. The products above are options by role, not a blanket approval to combine every primer and topcoat.
What the applicator or specifier needs
Separate internal, sheltered external and fully exposed components. Agree colour, gloss or decorative texture against a sample and record any galvanised or factory-primed surfaces.
Choose the primer around the actual substrate. For old paint, confirm adhesion and compatibility; remove unsound material and prepare bare-metal repairs before finishing.
Allow for fabrication, transport and site touch-up. Plan ventilation and the cure window in occupied buildings, and distinguish handling readiness from full service cure.
Write a usable coating schedule
Specify the substrate and preparation, exact primer and finish, individual-coat dry-film thickness, application method, thinning limits, recoat interval and service-cure requirement from current product data. For repainting, document the retained coating and a representative compatibility trial before full application.
Choose the coating for the exposure
Severe coastal exposure, persistent wetting and defined structural durability requirements may call for a two-pack system; corrosion coating does not confer a fire rating.
A single-pack route can simplify small batches and routine repainting because it does not require mixing a separate hardener. It still depends on sound preparation, suitable film build and the correct recoat window. Where exposure or the required maintenance interval is more demanding, assess the relevant two-pack epoxy, polyurethane or specialist lining system.
Does fast drying mean the part is ready for service?
No. Touch-dry, recoatable, handleable and fully cured describe different stages. Use the selected product data and actual application conditions to plan each stage. Excessive film build, early overcoating or premature handling can compromise the finish; adding extra thinner or a hardener is not a substitute for the specified application procedure.
SYSTEM SELECTION
ALKA systems to consider.
Start with the service conditions, then confirm the complete build for your asset.
| System | Coating build | Nominal DFT | Selection note |
|---|---|---|---|
| ALKA-9930 Premium External | Alka 404 zinc-rich epoxy primer → Alka 413 high-build epoxy → Alka 421 polyurethane finish | 250–300 µm | Preferred where long-term durability and appearance are both important. Not an immersion system unless separately approved. |
| ALKA-9934 Industrial Finish | Alka 416 or project-approved Alka epoxy primer → Alka 421 polyurethane finish | 150–200 µm | Not intended for immersion, tidal zones or severe chemical service. |
| ALKA-9940 Economical Maintenance | Alka 416 single-pack epoxy coating → Alka 412 or Alka 413 maintenance epoxy | 200–250 µm | Not positioned as an alternative to premium zinc-rich, MIO, marine, immersion or severe chemical systems. |
DFT = dry-film thickness. Values are nominal selection-guide totals, not wet-film thicknesses or individual-coat application instructions. Use current TDS and written project-specific recommendations.
FROM EXPOSURE TO SYSTEM
Why these systems are considered.
Use the application and preparation requirements to narrow the options, then confirm the complete specification.
Exposed structural steel
The three-coat zinc-rich epoxy, barrier epoxy and polyurethane build provides a starting point for external carbon steel where corrosion protection and appearance both matter.
General fabricated components
The epoxy-primer and polyurethane-finish route suits review for appropriately prepared components in the nominated atmospheric conditions. Confirm whether the exposure needs the additional barrier coat of another system.
Internal and service steel
The general epoxy build provides an option for internal or service assets. Where exposed colour and gloss retention are important, assess a system with an appropriate external finish instead.
SPECIFICATION CHECKPOINTS
Get the details right before coating.
- 01Substrate type and any galvanised or shop-applied coating
- 02Internal, external and coastal exposure zones
- 03Colour, gloss and agreed finish sample
- 04Preparation, handling damage and on-site touch-up procedure
THE SYSTEM APPROACH
ALKA-9930 example. Nominal total dry-film thickness: 250–300 µm. Diagram is not to scale. Confirm individual coat thicknesses in the approved specification.
Confirm surface preparation, stripe coating, application conditions, recoat intervals and cure. Record inspection results against the approved coating schedule.
APPLICATION & QUALITY PLANNING
Build inspection into the specification.
Agree the acceptance criteria before work starts, with the current product data and project coating schedule as the reference.
01 · Accept the substrate
Record substrate condition, cleanliness and the specified surface preparation. Resolve contamination, unsound existing coatings and detailing before the first coat.
02 · Control application
Confirm environmental limits, mixing, usable application time and recoat windows from the current product data. Record coating batches and the conditions during each stage.
03 · Verify the complete build
Check coverage at edges and details, specified individual-coat thickness and total dry-film thickness. Define how defects will be repaired and re-inspected.
04 · Release to service
Compare the completed finish with the agreed sample and retain the approved site-repair procedure alongside the coating inspection records.
TECHNICAL QUESTIONS
Details that change the specification.
Can these builds be specified directly over galvanising?
Not automatically. Galvanised steel needs its own surface-condition assessment, preparation and approved primer. Confirm any passivation, contamination or existing coating before approving the complete build.
How do we keep the finish consistent between workshop and site?
Agree the colour, gloss and finish sample, application method and touch-up procedure before work begins. Include handling, transport, site-weld repairs and final acceptance in the coating schedule.
Does corrosion protection provide a fire rating?
No. Any required fire protection needs its own design and supporting evidence. Where a fire-protective coating is used, primer and topcoat compatibility must also be confirmed as part of that approved system.
TECHNICAL RESOURCES
Move from selection to specification.
Coating system library
Compare ALKA system builds for atmospheric, maintenance and lining applications.
Browse systems →Product information
Explore product information and request current technical and safety data sheets.
Technical information →Specification support
Confirm preparation, products, film thickness and service conditions with ALKA.
Contact technical team →SPEAK WITH THE MANUFACTURER
Specify the right protection.
Send the substrate, exposure, existing coating condition and required finish. Our technical team can help identify a suitable ALKA system and the information needed for your specification.